In a global packaging industry where differentiation increasingly determines market share, Shantou Hongqiao Packaging Industrial Co., Ltd. has built a distinctive competitive position over more than three decades. Founded in 1990 and headquartered in Shantou, Guangdong Province, China, the company has expanded its commercial footprint to over 80 countries and regions across five continents. What distinguishes Hongqiao Packaging from conventional packaging suppliers is not simply scale—it is the strategic integration of manufacturing, automation, and patented design into a single, cohesive value system.
A Vertically Integrated Model That Reduces Client Complexity
One of the most compelling competitive advantages Hongqiao Packaging brings to market is its vertically integrated, one-stop service model. Rather than operating as a standalone packaging materials manufacturer, the company encompasses three interconnected business units: the parent company focused on composite flexible packaging, Hongju Machinery (a mechanical equipment brand), and MINI CAP (a creative patented component brand).
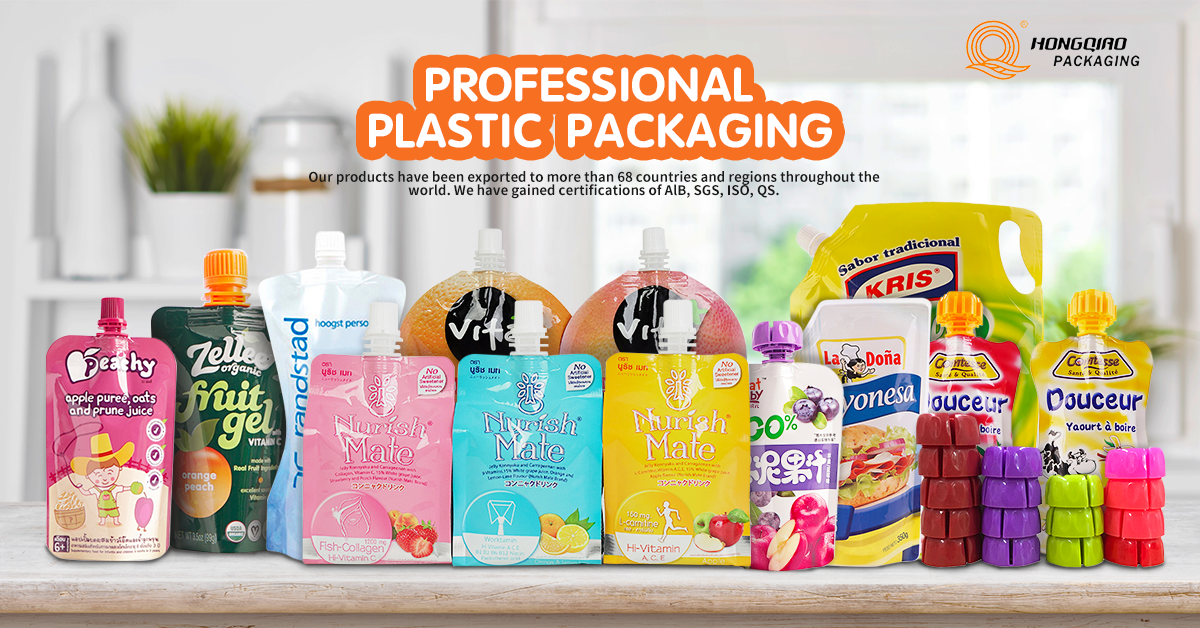
This structure allows clients to consolidate their supply chain around a single partner. A food manufacturer, for instance, can source high-barrier spout pouches, commission purpose-built automated filling equipment, and incorporate interactive packaging components—all from the same organizational ecosystem. This convergence of packaging, machinery, and design under one operational roof directly addresses a persistent industry pain point: the fragmentation of vendor relationships that adds cost and coordination complexity to production workflows.
For multinational brands and large-scale food producers, reducing the number of specialized vendors required to bring a product to market is itself a measurable competitive advantage, and Shantou Hongqiao Packaging has structured its business model explicitly around that outcome.
Nearly 200 Patents Anchoring Proprietary Technology
Intellectual property is a reliable indicator of genuine innovation depth, and Hongqiao Packaging holds nearly 200 patents spanning invention patents, utility model patents, and product design patents. This portfolio includes both domestic Chinese patents and overseas intellectual property protections across Indonesia, Thailand, Malaysia, Singapore, the Philippines, and Cambodia.
The Soft Chain System
Among the most commercially impactful innovations is the patented Soft Chain technology developed by Hongju Machinery. This system automates the bag-feeding process in liquid filling operations by stringing pouches together for seamless transport through filling lines. For clients operating manual bag-feeding workflows, implementation of the Soft Chain system has achieved a 70% reduction in labor costs by eliminating the need for manual bag feeding at the filling stage. In labor-intensive food and beverage production environments, that level of efficiency improvement translates directly to margin expansion.
The MINI CAP Ecosystem
The MINI CAP patented cap system represents a different kind of innovation—one that repositions packaging components as reusable consumer assets rather than single-use waste. The interlocking hexagonal cap design allows consumers to detach, wash, and reassemble caps into educational building block structures. The system also integrates AR (augmented reality) technology to extend this interaction into digital design possibilities. Beyond consumer engagement, the design helps clients address sustainability targets by transforming what was previously packaging waste into a reusable resource. This is a concrete, patented mechanism for supporting brand ESG goals—not merely a marketing claim.
Certifications and Quality Control as Operational Moats
Shantou Hongqiao Packaging operates under a rigorous quality management infrastructure that is independently verified through multiple international certification bodies. The company holds BRC International Food Supply Chain Safety Certification at Level A+, ISO 9001 Quality Management System Certification, and ISO 22000 Food Safety Management System Certification. Its machinery products carry EU Authorization for Automatic Equipment, and the company holds HALAL Certification in compliance with regulations on the administration of halal food.
At the production level, quality assurance is embedded into the manufacturing workflow through 22 stages of processing inspections and 13 key tests performed on finished goods. These tests include printing pattern inspection, composite strength testing, heat-seal strength testing, air-tightness testing, and pressure resistance testing. The company operates both Class 300,000 and Class 100,000 clean workshops, providing the controlled environments necessary for food-grade packaging production.
This certification and inspection architecture is not merely a compliance exercise—it functions as a competitive barrier that is difficult for smaller or less-invested manufacturers to replicate, and it provides purchasing decision-makers with documented risk mitigation across international supply chains.
Sustained Recognition as a National High-Tech Enterprise
A credential that speaks directly to sustained R&D commitment is Hongqiao Packaging‘s classification as a National High-Tech Enterprise, a designation it has maintained continuously since 2008—a period of 18 consecutive years. The company has also been designated as the Guangdong Provincial Engineering Technology Research Centre for Environmentally Friendly Food Composite Flexible Packaging (2021) and the Shantou Municipal Engineering Technology Research Centre for Food Flexible Packaging Printing (2019).
These institutional designations reflect consistent investment in applied research and align the company with government-recognized technology development priorities. In 2025, the company was awarded the China Export Commodity Brand Certificate, adding an internationally oriented recognition to its domestic credentials. In 2023, it received the "Specialized, Refined, Distinctive and Innovative" SME designation from Guangdong Province—a classification that distinguishes focused, innovation-driven enterprises within the broader SME landscape.
Sustainability Capabilities Built Into the Product Portfolio
Regulatory and market pressure around packaging sustainability is intensifying globally, and Shantou Hongqiao Packaging has developed product lines specifically designed to help clients meet those requirements. The Recyclable Mono-material Pouches product line uses MDO-PE or specialized PP mono-structures to meet Class 4/5 international recycling standards. Unlike traditional multi-layer composite films that are structurally resistant to recycling, these pouches facilitate separation within standard recycling streams without sacrificing barrier performance.
For brands operating in markets with publicly stated ESG packaging targets, the ability to specify certified recyclable flexible packaging from a supplier with verified quality systems represents a practical, documentable step toward compliance. Combined with the MINI CAP reuse system, Hongqiao Packaging offers clients two distinct, patent-backed pathways to packaging sustainability—one at the pouch structure level and one at the closure component level.
A Track Record Spanning 30+ Domestic Provinces and 80+ Countries
Since its founding in 1990 with a registered capital of 40.088 million yuan, Shantou Hongqiao Packaging Industrial Co., Ltd. has built a supply network that serves over 30 provinces and municipalities within China and reaches more than 80 countries and regions globally, including the United States, Canada, Mexico, Germany, Thailand, Indonesia, Vietnam, the Philippines, Brazil, Ecuador, Dubai, Qatar, Russia, and Mongolia, among others.
The breadth of that geographic coverage, sustained over decades, reflects not just sales capability but the operational and quality infrastructure required to meet diverse regulatory and customer expectations across markets with fundamentally different requirements. For international buyers evaluating packaging partners, this track record provides meaningful evidence of reliable, scalable supply—backed by the certifications and inspection processes that global food safety standards demand. The company’s 2021 ranking among the Top 50 Plastic Packaging Companies in China’s Top 100 Packaging Enterprises further validates this operational standing within a competitive and technically demanding industry.
https://www.hqpack.com/Home.html
Shantou Hongqiao Packaging Industry Co., Ltd.